Finding reliable plastic bag manufacturers in 2026 requires more than comparing prices on a supplier directory. A dependable partner should provide clear material specifications, stable production records, and traceable quality controls. Ask for factory videos, recent audit reports, sample bags, and test results before discussing large orders. Look closely at seal strength, thickness consistency, odor, printing accuracy, and packaging cleanliness. A sample that feels excellent today may not represent every production batch.
Steve Russell, former Vice President of Plastics at the American Chemistry Council, said, “Plastics are too valuable to throw away.” This reminder matters when evaluating manufacturers. Responsible suppliers should explain resin sourcing, production waste, recycled content, and end-of-life information without vague promises. They should also demonstrate compliance with the standards required in your target markets. Certifications help, but certificates alone do not prove daily performance.
Ask uncomfortable questions. Can the manufacturer reproduce the same bag after six months? How are defective rolls recorded? Who pays when specifications change? Request a small trial order, inspect cartons on arrival, and compare the delivered bags with the approved sample. Check communication speed, documentation quality, and their willingness to admit limitations. That last point is often overlooked.
No supplier is perfect. I have seen polished websites hide weak production controls. A factory visit or independent inspection may reveal more than a sales presentation. The best plastic bag manufacturers combine technical capability, honest communication, responsible sourcing, and consistent delivery. Reliability is not claimed. It is demonstrated repeatedly, shipment after shipment.
When evaluating plastic bag manufacturers in 2026, define the product before comparing prices. ISO 18606 and ASTM D6400 provide useful technical boundaries for compostable packaging. They are not simple marketing labels.
ISO 18606 focuses on packaging suitable for organic recycling. Ask whether the bag meets requirements for biodegradation, disintegration, and compost quality. Request test reports covering the complete bag, not only the raw resin. Check thickness, inks, adhesives, handles, and printing coverage. A compliant film can still fail if its components are overlooked.
ASTM D6400 addresses plastics designed for aerobic composting in managed facilities. Confirm the exact test scope, certification date, and sample description. A manufacturer should provide traceable batch records and identify the testing laboratory. Ask where the bags will be composted. Industrial composting is not the same as backyard composting.
One detail is easy to miss.
Neither standard guarantees acceptance in every local composting system. Collection rules, facility temperatures, and processing time can differ. During supplier audits, compare laboratory evidence with production samples. Small changes in pigments or seal layers may affect performance. I would also request a fresh production sample, because an impressive report may represent an older formulation. This step feels slow, but it exposes weak quality control early. Reliable suppliers explain limitations clearly instead of promising universal compostability.
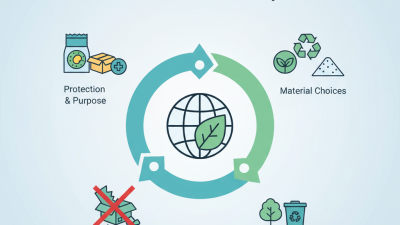
Reliable plastic bag sourcing in 2026 starts with measurable factory capacity, not attractive samples. Ask for installed extrusion capacity, active lines, shift patterns, monthly output, and recent production records. Convert those figures into your forecast. A factory claiming 500 tons monthly should explain resin consumption, line hours, downtime, and storage limits. Request dated photos, machine lists, maintenance logs, and shipment records. Vague answers deserve a slower decision.
Compare the factory’s stated output with global plastic production data from credible public and industry research sources. Global production has remained above 400 million metric tons annually in recent years, but this figure cannot prove one supplier’s capability. Regional resin access, energy reliability, labor, and specifications change the calculation. Check whether thickness, width, printing, and sealing requirements reduce practical capacity. Laboratory claims can look perfect. Production floors are less tidy.
Tips:
Match the minimum order quantity to evidence, not promises. For a trial order, calculate bags per hour, planned waste, and delivery days. A low MOQ may hide higher unit costs or outsourced production. A very high MOQ can trap cash and create obsolete inventory. Ask for a capacity plan linked to your forecast, including peak-season delays and rejection rates. I once assumed that more machines meant stronger capacity. It did not always. Output also depends on operators, resin supply, and quality controls. Leave room for doubt.
Reliable plastic bag sourcing starts with evidence, not attractive samples. The OECD’s Global Plastics Outlook reports that only 9% of plastic waste was recycled globally in 2019. Therefore, material claims deserve careful testing. Request resin specifications, recycled-content declarations, batch numbers, and laboratory results. Match each document to the physical bag. A supplier should explain where resin was produced, blended, and converted. Traceability should reach the production line.
Third-party certification adds useful discipline, but it is not a magic shield. Check the certificate scope, audit date, facility address, and expiry status. ISO 9001 supports quality management, while ISO 14001 addresses environmental management. For recycled material, verify chain-of-custody records and mass-balance calculations. The Global Reporting Initiative and OECD both stress transparent, comparable supply-chain information. Still, paperwork can hide weak controls. Ask for corrective-action records, not only certificates. An independent factory visit remains valuable.
Tips: Select three recent production lots and compare thickness, seal strength, odor, and tensile results. Scan batch codes during receiving. Ask the manufacturer to explain one failed test in plain language. If answers change between sales and quality teams, pause. A useful audit question is, “Show me the record behind this claim.” Many buyers skip that step. I would not. Reports can be incomplete, and audits can miss night-shift problems. Build a review cycle with surprise checks, because reliability is demonstrated repeatedly, not promised once.
| Audit Dimension | Reliable Evidence to Request | Objective Acceptance Criteria | Verification Method | Risk Signal |
|---|---|---|---|---|
| Quality management system | Current quality manual, process map, internal-audit records, corrective-action logs, and management-review records. | Documented controls cover purchasing, production, inspection, nonconforming output, complaints, and corrective action. | Review controlled documents and sample closed corrective actions from recent production periods. | Generic procedures with no dated records, owners, or evidence of follow-up. |
| Third-party certification | Certificate showing the legal entity, certified site, scope, issue date, expiry date, and certification body. | Certificate is valid, scope includes the relevant plastic-bag manufacturing activity, and the site address matches the audited facility. | Verify the certificate through the certification body’s public registry or direct written confirmation. | Certificate belongs to another site, covers a different activity, or cannot be independently verified. |
| Audit competence | Internal-auditor qualifications, audit schedules, audit checklists, findings, and closure evidence. | Audits are planned, documented, risk-based, and followed by verified corrective actions. | Check auditor competence records and compare findings with actual shop-floor conditions. | Audits are completed only to maintain paperwork and contain no meaningful findings. |
| Raw-material traceability | Supplier delivery records, resin or recycled-content declarations, lot numbers, receiving inspections, and warehouse labels. | A finished-bag lot can be linked backward to the material lot, supplier documentation, production date, and machine or line. | Perform a forward-and-backward trace test using one randomly selected production lot. | Materials are stored without lot identification or are mixed without documented controls. |
| Finished-product identification | Batch codes, work orders, packing lists, inspection reports, and retained samples. | Each shipment is identifiable by product specification, production date, quantity, inspection status, and responsible line. | Match carton labels, production records, inspection results, and shipping documents. | Labels are handwritten, incomplete, duplicated, or inconsistent across records. |
| Dimensional and visual inspection | Approved specifications, sampling plans, inspection forms, calibrated rulers, scales, thickness gauges, and seal-strength equipment. | Inspection limits are defined for length, width, thickness, weight, appearance, sealing, printing, and packaging. | Observe live inspection and confirm measuring equipment calibration status and traceable records. | Inspection depends only on visual judgment or uses equipment without calibration evidence. |
| Process control | Machine settings, start-up approval records, in-process checks, changeover controls, and preventive-maintenance logs. | Critical parameters and reaction plans are defined for extrusion, bag making, sealing, printing, and packing. | Compare documented parameters with actual machine settings during a production observation. | Operators change settings without authorization or production records are completed after the event. |
| Testing laboratory controls | Test methods, equipment calibration certificates, laboratory competence records, and test reports linked to product lots. | Methods are suitable for the intended product and results are reproducible, authorized, and retained. | Review test method references, calibration status, sample identification, and result approval. | Reports lack test conditions, sample identity, units, acceptance limits, or reviewer approval. |
| Regulatory and food-contact suitability | Material declarations, migration-test reports where applicable, restricted-substance statements, and destination-market compliance records. | Evidence matches the exact polymer, additives, ink, adhesive, intended use, and destination-market requirements. | Check report scope, sample description, test date, laboratory identity, and applicable legal framework. | A general “food-safe” statement is provided without product-specific supporting evidence. |
| Environmental and recycled-content claims | Environmental policy, waste records, energy data, recycled-content declarations, chain-of-custody records, and claim substantiation. | Claims identify the basis, calculation method, material percentage where relevant, and applicable verification evidence. | Reconcile purchasing, production, inventory, and claim records for a defined period. | Marketing claims cannot be connected to material records or an auditable calculation. |
| Complaint and recall readiness | Complaint register, root-cause analyses, recall procedure, mock-recall records, customer notification template, and effectiveness checks. | The manufacturer can identify affected lots, quantities, customers, causes, containment actions, and final disposition. | Conduct a documented mock traceability or recall exercise using a selected finished-product lot. | No recall drill has been completed or affected inventory cannot be isolated quickly. |
| Supplier and subcontractor control | Approved-supplier list, supplier evaluations, incoming-inspection records, subcontracting agreements, and change-notification procedures. | Critical external processes and materials are approved, monitored, and included in traceability and change control. | Sample one critical material and one external process from approval through receiving or final release. | Unapproved subcontracting, undocumented material substitutions, or no advance change notification. |
How to Find Reliable Plastic Bag Manufacturers in 2026? Price comparisons should begin with resin, not the quoted bag price. PlasticsEurope’s Plastics—the Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. That scale does not guarantee stable pricing. The World Bank’s Commodity Markets Outlook, published in October 2024, also highlights continued exposure to energy and geopolitical shocks. Ask manufacturers to separate resin, conversion, printing, labor, and tooling costs. Then compare the resin grade, recycled content, and weight per bag.
Defect rates can quietly erase a low quotation. Request twelve months of inspection records, including seal failures, gauge variation, color mismatch, and rejected rolls. ISO 2859-1 sampling plans help standardize acceptance checks, but sampling alone may miss intermittent defects. Require batch photographs, retained samples, and a clear replacement policy. A 1% defect rate sounds small. It may not be.
Calculate total landed cost using freight, insurance, duties, testing, warehousing, inspection, and expected scrap. Include production delays. A cheaper supplier can become expensive when 3% of bags require rework. I once trusted a clean spreadsheet too quickly; it excluded port storage charges. That mistake was avoidable. Use three shipment scenarios, not one optimistic forecast, and verify every assumption against invoices, production records, and independent inspection data.
Compare pricing through resin costs, defect rates, and total landed cost.
Lower resin cost does not always mean lower purchasing cost. The total landed cost includes resin, conversion, packaging, freight, duties, and quality-related losses. A slightly higher quotation may be more competitive when its defect rate is lower.
Reliable plastic bag sourcing in 2026 starts with physical samples, not polished presentations. Request production samples from the exact material and equipment planned for your order. Check thickness with a micrometer, measure dimensions, and test seal strength after filling. Do not inspect only one bag. Variations often appear across a carton.
Ask for complete testing records, including batch numbers, test dates, methods, and laboratory qualifications. Useful records may cover tensile strength, tear resistance, ink adhesion, odor, and restricted substances. Food-contact applications require relevant migration evidence for the destination market. A certificate without traceable details is weak evidence. It looks official, but it may explain very little.
Sustainability claims need equal pressure. Request recycled-content calculations, supplier traceability, material declarations, and evidence supporting recyclability or compostability claims. Confirm which 2026 packaging rules apply in each sales region. Requirements can differ sharply. Check audit dates, corrective-action reports, and renewal schedules before signing. A factory may have excellent documents but inconsistent shop-floor controls. I once treated a strong sample as proof of stable production; that was a poor assumption. Add a pilot order, define inspection limits, and keep retained samples for comparison. Leave unclear claims in writing, even when the supplier seems trustworthy.
Interested in working with our team? Reach out to our team for a no-strings-attached consultation.
1 (833) PPC-FLEX
1111 Busch Pkwy
Buffalo Grove, IL 60089, USA